
Tradeshow: SchraubTec 2026
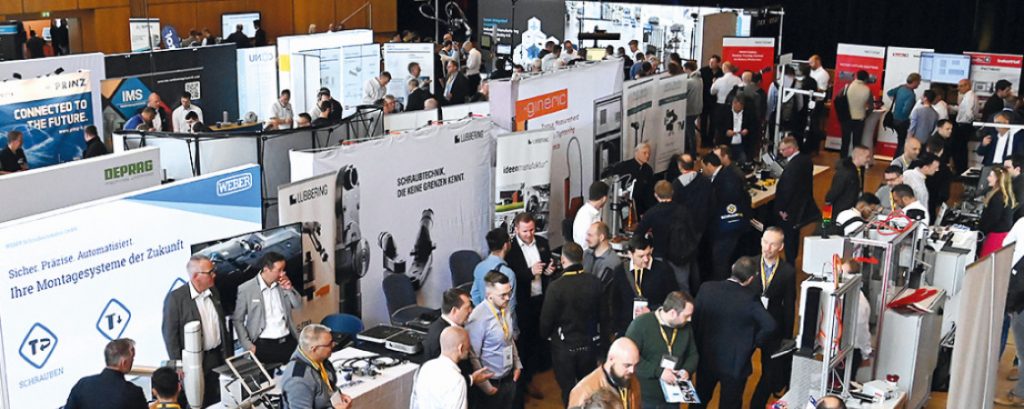
Expanite exhibiting at SchraubTec 2026
Date: April 16, 2026
Location: Stuttgart, Germany
Booth number 38
We look forward to connecting with you at SchraubTec 2026!
Date: April 16, 2026
Location: Stuttgart, Germany
Booth number 38
We look forward to connecting with you at SchraubTec 2026!

Article from Valve World:
With the EU’s 2024 ban on hard chrome plating, the valve industry faces urgent change. This article explores the environmental, technical and compliance challenges of chrome plating, and how Expanite offers a cleaner, high-performance alternative without hazardous chemicals.

The main concerns about hard chrome plating
For decades, hard chrome plating has been the standard surface treatment in the valve industry, improving wear and galling resistance. However, hard chrome plating was officially banned by the EU in 2024. The process involves the use of hazardous chemicals containing hexavalent chromium and requires post-processing like grinding and polishing. Hexavalent chromium is widely banned under the REACH regulation. The use of hexavalent chromium, a known carcinogen, creates significant environmental and health risks, while issues such as cracking, pitting and poor adhesion can compromise the functionality of the plated components. Under the RoHS (Restriction of Hazardous Substances) Directive, the use of hexavalent chromium is generally not compliant. Therefore, manufacturers now push for a cleaner, more sustainable alternative for hardening their parts without compromising performance.
Expanite®: An alternative to hard chrome plating
The patented Expanite technology is different to the electrochemical process of hard chrome plating as it is a gas-based process taking place in electric furnaces and what is more, it’s not a coating. Expanite does not use any hazardous materials or chemicals, thus, there is no outlet of any chemicals.
Expanite treatment is what specialists call a “thermo-chemical conversion”, or in simpler terms, a diffusion-based surface hardening process. The product which Expanite offers as a substitute for hard chrome plating on austenitic alloys consists of two process steps. The first step is ExpaniteHigh-T, a vacuum solution nitriding process that anneals the core material and provides limited increase in surface hardness, in relation to the core. The second step, ExpaniteLow-T creates a conversion layer of expanded austenite. No material is added or deposited on top of the surface of the parts, but rather a solid solution of interstitially dissolved large amounts of nitrogen, and carbon atoms are created thanks to precise control of process parameters. Those interstitial atoms occupy octahedral interstices of the crystal lattice and are responsible for inducing local strain fields, thereby generating compressive stresses in the affected region. As a result we see an increase in hardness of up to ten times, and with it, improved wear, galling and other mechanical properties.
The SuperExpanite process does not require extensive pre-processing steps, which are traditionally used to remove the passive layer, prohibiting absorption of atoms from the process atmosphere. The passive oxide layer is a natural protection barrier on top of the surface of stainless steels and is impenetrable to atoms. In the Expanite process, the passive oxide layer is reduced in-situ during treatment utilizsing the same process atmosphere. After processing, the surface is exposed to atmospheric air and re-passivates, keeping the corrosion resistance properties of the material. Due to Expanite being a gas-based process, the uniformity of coverage is not limited by complicated geometries. Moreover, the lack of post-process finishing, like grinding and polishing, makes the overall treatment significantly simpler and shorter, and the final geometry of products is more stable. What Expanite achieves is a high hardness (up to 1300HV) on the surface, which is equivalent to, or even harder than hard chrome plating. The depth of the treatment varies and is dependent on final application, however, usual values lie within 10-30µm. Expanite is bringing protection to the component and extending the life of the component.
Technical aspects of moving away from hard chrome plating
There is a huge benefit of not using coating processes within the valves and other components because you avoid the delamination from the surface. There are many different chemical processes that do not allow hard chrome usage because of process media reacting with chrome in the coating. Common processes in the chemical industry containing any of these media would react with the chrome and dissolve the plating: hydrochloric (muriatic) acid, hydrofluoric acid, liquids with chloride salts, sulphuric acid (especially if heated), phosphoric acid and nitric acid (attacked slowly). Processes where the risk of the hard chrome layer peeling off and contaminating the media can become dangerous, such as in the fibre suspension, food, beverage and medical industries. In standardised tests, Expanite treatment lowers the wear rate of the austenitic stainless steels over 100 times, as compared to the untreated material. This improvement can be attributed to the surface hardness increase of a factor of 5-10 depending on the base material (up to 1300HV0.05). The standard treatment depth of 20µm provides protection against wear even when hard third body particles are present. This increase in hardness is also responsible for significant improvement in resistance to adhesive wear. The risk of cold welding and of its dynamic form known as galling are mitigated beyond the yield strength of the austenitic stainless steels, which allows for smooth operations of valve components, even under high loads and after long periods without operation. One of the advantages of the Expanite treatment is the improvement of pitting corrosion resistance of austenitic components treated with SuperExpanite. Thanks to the nitrogen dissolved in the surface, the PREN number goes up, and with it, the breakdown potential, meaning that the surface stays passive beyond what is possible for the untreated material.
Applying Expanite
Ramén Valves made the switch to the Expanite technology for various reasons, including the environmental benefits, chemical composition and corrosion and wear resistance. Compared the hard chrome plating, Expanite has been able to offer a higher performance in terms of corrosion resistance and wear compared to hard chrome plating, as well as a better environmental impact as the company’s valves are now treated without the use of toxic chemicals.

Booth in the Danish pavillon: LU8559
Date: October 18-21, 2026
Location: Chicago, Illinois, USA
Free registration using Comp Code 77U32 here

Expanite invited to speak at IMAT
Date: Thursday, October 23, 2025: 11:50 AM
Locations: 140G (Huntington Place Convention Center)
Our CTO Thomas Strabo Hummelshøj will be speaking about the subject “Low-temperature stainless steel & Titanium surface hardening” – lead more here


Language: English – German – Italian – French please sign up below:

As the first company in the surface hardening and heat treatment industry, Expanite has completed an independently verified Life Cycle Assessment (LCA) that documents the environmental footprint of its hardening technologies. The results confirm what Expanite has long claimed that its processes have a low climate impact thanks to a low CO2 footprint and no use of toxic materials.
The findings of the LCA were very positive. The climate impact of Expanite’s processes on stainless steel surface hardening leads to only 0,23-0.46 kg CO2 eq per kg of treated material. When compared to the 10.5 kg CO2 eq/kg emissions of untreated stainless steel, the Expanite process adds only 2-14% of greenhouse gas emissions. This very low impact justifies investing or switching to Expanite is environmentally responsible and economically sound. The LCA documents that the Expanite processes are free from fluoride, hydrochloric acid and/or cyanides. The processes generate no toxic waste and, perhaps even more importantly, do not use solvents. The soot emissions from the Expanite processes are so low that there are no health risks. All Expanite sites are fully compliant with local and national environmental standards.

Too much talk – too little data. That’s how Expanite, the surface hardening specialist, sums up the state of sustainability in the heat treatment industry. But now, Expanite is changing that narrative. As the first company in the surface hardening and heat treatment industry, Expanite has completed an independently verified Life Cycle Assessment (LCA) that documents the environmental footprint of its hardening technologies. The results confirm what Expanite has long claimed: that its processes have a low climate impact thanks to a low CO2 footprint and no use of toxic materials.
“When we started the project of documenting our CO2 footprint for the Expanite processes, we quickly realised that while there was plenty of talk and flashy PowerPoint presentations out there, actual data is not available”, says Thomas Sandholdt, CEO of Expanite. “We believe transparency builds trust, especially in an industry that has traditionally not been very open. We know from discussions with our customers that compliance is a big challenge, as data is hard to come by. That is why we commissioned an independent EU-based consultancy company to conduct a full LCA of our processes, documenting our environmental footprint.”
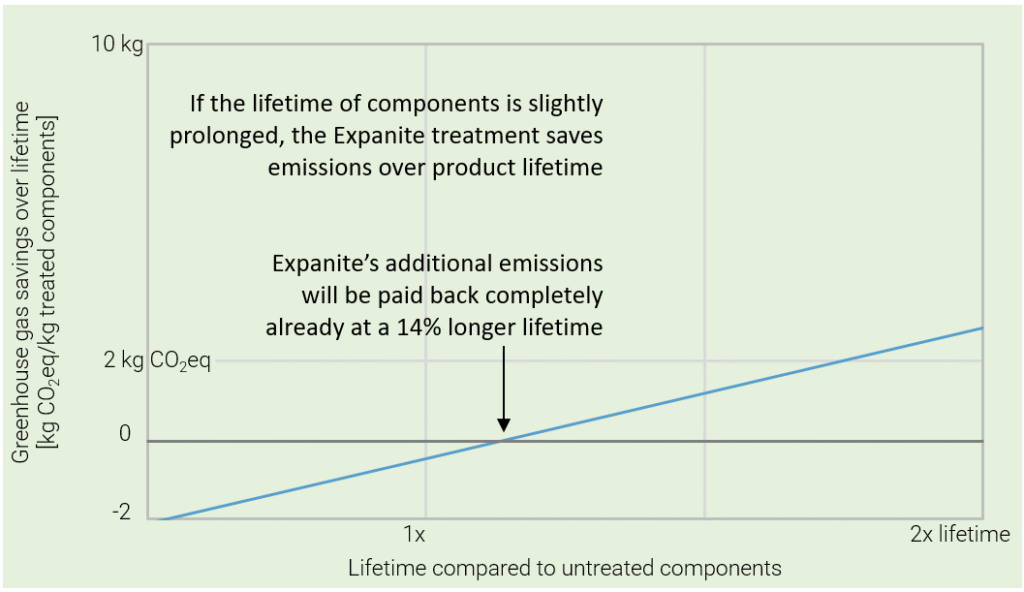
The findings of the LCA were very positive. The climate impact of Expanite’s processes on stainless steel surface hardening leads to only 0,23-0.46 kg CO2 eq per kg of treated material. When compared to the 10.5 kg CO2 eq/kg emissions of untreated stainless steel, the Expanite process adds only 2-14% of greenhouse gas emissions. This very low impact justifies investing or switching to Expanite is environmentally responsible and economically sound. The LCA documents that the Expanite processes are free from fluoride, hydrochloric acid and/or cyanides. The processes generate no toxic waste and, perhaps even more importantly, do not use solvents. The soot emissions from the Expanite processes are so low that there are no health risks. All Expanite sites are fully compliant with local and national environmental standards.
“We know from our market research that sustainability, including decarbonization, is increasing in importance when selecting suppliers. Transparency has always been at the core of our business. Our doors are open, and customers are always welcome to visit our treatment centers around the globe. Expanite was born out of a wish to provide a more sustainable heat treatment solution. We challenge the industry: ask your current suppliers to provide data on their heat treatment solution. If they cannot show you documentation, maybe it is time to talk to Expanite,” says Thomas Sandholdt with a smile.
Expanites sustainable advantages are not only about carbon footprint. By combining the two process steps, Expanite eliminates the so-called eggshell effect, which occurs in most surface hardening methods. This gives you a superior material performance for numerous applications, including pumps and valves for the food processing industry. Other applications that enjoy the uniform benefits of improved wear, galling and corrosion are Automotive, Oil & Gas, Marine and many others.
Expanite offers state-of-the-art solutions for surface hardening treatment of stainless steels and titanium.
With Expanite’s processes, it is possible to increase the material’s surface hardness tenfold while at the same time maintaining and even increasing its corrosion resistance. Expanite is a global organization with a combined development and production facility near Copenhagen, Denmark, and hardening capacity in both US, Germany, Korea and China. Expanite’s solutions are flexible and can be introduced directly into a customer’s own production line as part of a licensing arrangement. Learn more on www.expanite.com.

As the days get longer and brighter, we bring you fresh insights into how Expanite continues to push the boundaries of material surface hardening.
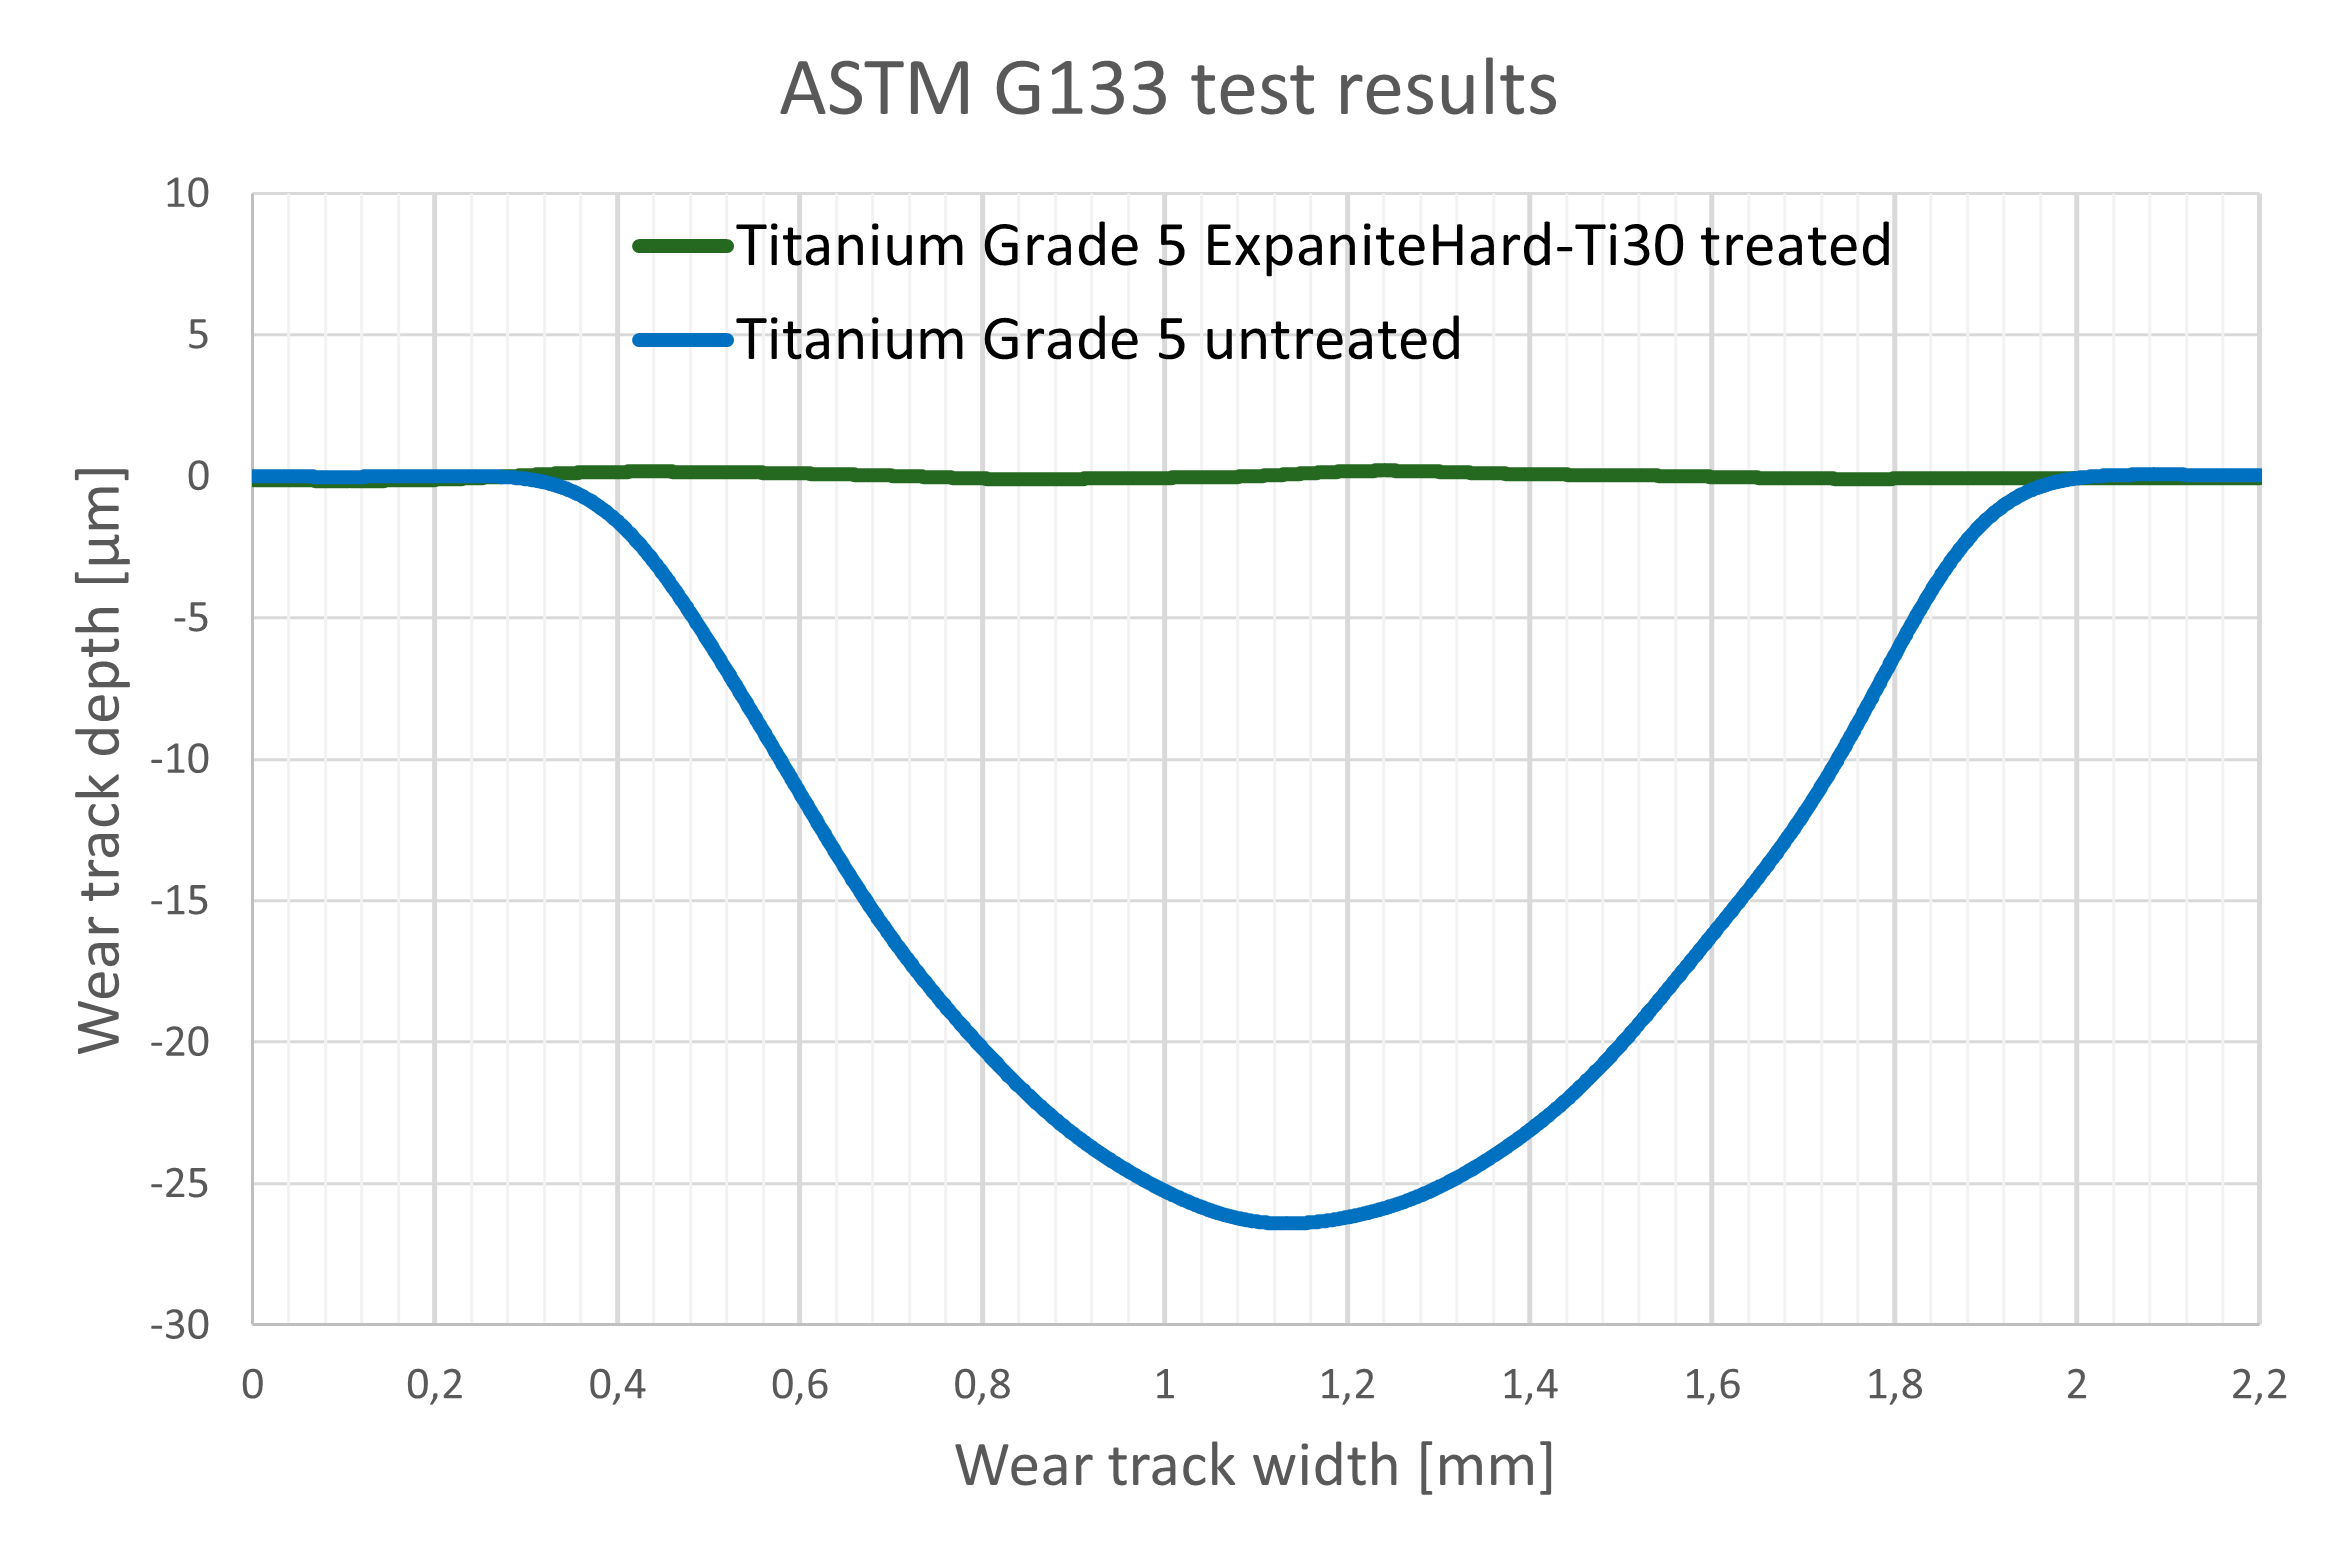
In this newsletter, we share insights on how our ExpaniteHard-Ti process achieves an industry-leading 370x wear resistance improvement for Titanium Grade 5.
You will also get to know more on our CTO, Thomas Strabo Hummelshøj, in our “Meet the Tech Team” series, explore why industries are moving away from hard chrome plating, and meet our newest colleagues across Europe and the U.S.
Finally, if sustainability is a priority for you, we offer full transparency on the environmental footprint of our processes with our independently verified LCA data.

Expanite® is expanding its U.S. Operations and Organization – adding signicant Heat Treatment Capacity and New Technologies! Expanite, the innovative heat treatment and surface hardening provider, is signicantly expanding its U.S. operations. As part of this strategic investment, Expanite is making its ExpaniteHard-Ti process for surface hardening of titanium available to North American customers, alongside the widely adopted SuperExpanite® processes enhancing wear, galling and corrosion resistance of stainless steel, nickel-based, and other specialty alloys. New Facility, Bigger Volumes, Larger Parts, and New Capabilities Expanite Inc., a subsidiary of Expanite A/S based in Denmark, is signicantly expanding its operations in North America with a major investment in a larger facility, tripling its heat treatment and surface hardening capacity.
Expanite Inc. is relocating to a new and larger facility in Twinsburg, Ohio and bringing in new furnaces to meet the growing demand for advanced surface hardening and heat treatment solutions across a wide range of industries. The new advanced furnaces – with chamber sizes up to 24x24x36” – are supplied and installed by Seco/Warwick. The new equipment will allow Expanite to process larger and more complex components while maintaining the unique hardening quality, widely accepted for improving product performance on stainless steel. The increased capacity and capabilities will further enhance the lead times and flexibility that Expanite is known for. This strategic expansion not only boosts Expanite’s ability to serve a growing number of industries such as pumps, valves, food & beverage processing equipment, medical devices and automotive, but also aligns with the company’s commitment to sustainability by offering greener alternatives to traditional technologies
“Our investment is all about meeting the growing demands from our North American customers,” says Thomas Sandholdt, CEO of Expanite. “We’re now able to handle much larger volumes while maintaining the fast lead times and flexibility that our customers expect from Expanite.” Expanite is bringing Patented Technology USA Commercial Heat Treater Expands for Hardening of Titanium to North America Expanite Inc. is now not only offering its well-known SuperExpanite processes for stainless steel but also its patented ExpaniteHard-Ti process — an advanced surface hardening solution designed for hardening of titanium parts.
Previously ExpaniteHard-Ti was only available from Expanite’s headquarters in Denmark. The ExpaniteHard-Ti process significantly improves wear and galling resistance, extending life and expanding the possible applications of titanium components. “Our expanded capabilities mean we can now offer our full range of Expanite technologies, including the processes for titanium, right here in the U.S.”, added Claus Løndal, Country Manager, North America “This allows us to serve a wide range of customers while reducing lead times and costs”. Expanding Heat Treatment Capabilities Besides the proprietary Expanite standard vacuum heat treatment processes are offered from Expanite.
This includes hardening of tool steels (D2, A2, M2, H13, etc.), austenite annealing of stainless (304, 316, etc.), precipitation treatment of PH-steels (17-4PH, 13-8PH, etc.) and specialty treatment of alloys (Inconel 718, MU-metal etc.). The addition of vacuum heat treatment solutions extends Expanite’s capabilities, offering more solutions, and greater flexibility and ensuring customers receive hardening solutions tailored to their specific needs. A Stronger Team, A Stronger Presence To support this expansion, Expanite Inc. has also strengthened its team with additional specialists in surface hardening and heat treatment, ensuring that the growing demand is met with the highest level of service and expertise while reinforcing the company’s commitment to sustainability and innovation.

Expanite offers an innovative technology that prevents wear, galling, and corrosion of components in stainless steel or titanium by hardening the material in a pure-gas environment without using harsh chemicals, leaving no toxic waste and with a low carbon footprint.
Hardening of parts such as gears and other essential products made from stainless-steel alloys is a vital and necessary process to ensure those parts perform optimally.
Expanite, a company that was born from research at The Technical University of Copenhagen, has grown its innovative process of hardening stainless steel more efficiently than previous methods.
Besides the proprietary processes for stainless steel and titanium, Expanite offers specialty heat treatment solutions including hardening, tempering, solution treatment, aging, and annealing for nickel-based alloys such Monel®, Inconel® or Mu-metal, stainless steels, titanium, and other specialty materials.
“You can easily take stainless steel and put it in and harden it, but you lose corrosion properties right away if you don’t know how to do it,” said Claus Løndal, country manager North America with Expanite. “We do that without losing corrosion properties.”
The beauty of Expanite’s hardening process is it works with any stainless-steel alloy, according to Løndal.
“We can take all stainless-steel alloys – and I mean every stainless-steel alloy, as long as they are defined as stainless steel,” he said. “That means that it has to have around 12 percent chrome in the alloy. And we can harden them all. We can also harden some other alloys and titanium.”
Stainless steel is an amazing material, according to Løndal, but it isn’t a very hard material.
“If you go out and — you probably have a refrigerator or a dishwasher that is a stainless-steel surface – and if you take a knife, you can scratch it, or you can scratch it with your fingers; that’s how soft it is,” he said. “We can harden it almost 10 times as hard as that in the surface. It’s a surface hardening of the material. Our advantage is that you don’t see a drop in corrosion properties after our process.”
Corrosion is a common problem when dealing with stainless steels, and — if not dealt with — can become a hazard for industries using food and beverage equipment or medical and aerospace sectors, according to Løndal.
“You don’t want your parts to corrode because, at some point, it will corrode so much that it goes to pieces,” he said.