(Articel auf English)
As the first company in the surface hardening and heat treatment industry, Expanite has completed an independently verified Life Cycle Assessment (LCA) that documents the environmental footprint of its hardening technologies. The results confirm what Expanite has long claimed that its processes have a low climate impact thanks to a low CO2 footprint and no use of toxic materials.
The findings of the LCA were very positive. The climate impact of Expanite’s processes on stainless steel surface hardening leads to only 0,23-0.46 kg CO2 eq per kg of treated material. When compared to the 10.5 kg CO2 eq/kg emissions of untreated stainless steel, the Expanite process adds only 2-14% of greenhouse gas emissions. This very low impact justifies investing or switching to Expanite is environmentally responsible and economically sound. The LCA documents that the Expanite processes are free from fluoride, hydrochloric acid and/or cyanides. The processes generate no toxic waste and, perhaps even more importantly, do not use solvents. The soot emissions from the Expanite processes are so low that there are no health risks. All Expanite sites are fully compliant with local and national environmental standards.
Expanite invited to speak at Schraubtec Stuttgart February 19, 2025
The SchraubTec conference is all about screw connections in industry. In practical lectures and the exhibition, you will strengthen your specialist knowledge and skills on this important topic.
Meet experts for screw connections, screw technology, screw tools as well as procurement, purchasing and management of C-parts. Get advice on current products and solutions for your screwing tasks.
Ein Jahr des Wachstums, der Innovation und der Nachhaltigkeit
„Sehr geehrte Kunden und Partner von Expanite,
zum Jahresende möchte ich die Gelegenheit nutzen, um auf ein ereignisreiches Jahr 2024 zurückzublicken und gleichzeitig einen Ausblick auf das vielversprechende Jahr zu geben, das vor uns liegt.
Das Jahr 2024 war in vielerlei Hinsicht spannend für Expanite. Trotz eines industriellen Umfelds, dass von Unsicherheiten zwischen Rezession und geringem Wachstum geprägt war, konnten wir erneut ein signifikantes Wachstum in unseren drei Kernregionen Asien, Nordamerika und Europa verzeichnen.
Unser deutlich spürbares Wachstum unterstreicht, dass immer mehr Kunden auf unsere nachhaltigen Lösungen setzen. Dieser Erfolg ist dem fortwährenden Vertrauen unserer treuen Kunden sowie der Zusammenarbeit mit neuen Partnern zu verdanken. Dafür möchten wir uns herzlich bedanken und versichern Ihnen, dass wir weiterhin mit vollem Einsatz daran arbeiten, uns kontinuierlich weiterzuentwickeln.
Einige Highlights aus dem Jahr 2024:
Investitionen in Nordamerika: Wir haben umfangreich in neue Anlagen investiert, wodurch wir unsere Kapazitäten weiter ausbauen konnten. Gleichzeitig wurde unsere ExpaniteHard-Ti-Technologie zur Titanhärtung erfolgreich in das US-Behandlungszentrum integriert.
Webinare und Messen: Mit über 20 Webinaren, an denen mehr als 300 Teilnehmer aus aller Welt teilnahmen, und einem starken Auftritt auf internationalen Messen in Europa, Nordamerika und Asien, haben wir Wissen geteilt und unsere Präsenz gestärkt.
Nachhaltigkeit und Lebenszyklusanalyse (LCA): Wir haben unsere Lebenszyklusanalyse (LCA) abgeschlossen – durchgeführt von unabhängigen Experten – und damit die CO₂- und Chemikalienbilanz unserer Prozesse dokumentiert. Damit sind wir vermutlich die Ersten in der Wärmebehandlungsbranche, die eine LCA anbieten, um unseren Kunden und Partnern maximale Transparenz zu bieten. Nachhaltigkeit ist und bleibt ein zentraler Bestandteil unserer Unternehmenskultur, und wir sind stolz darauf, dieses Thema weiter voranzutreiben..
Herbst-Updates: Expanites Wachstum, Nachhaltigkeitsinitiativen und Event-Highlights
Der Herbst naht, und bei Expanite gibt es aufregende Neuigkeiten, die wir Ihnen nicht vorenthalten möchten. In diesem Newsletter informieren wir Sie über die Erweiterung unseres Standorts in den USA, um der steigenden Kundennachfrage gerecht zu werden. Außerdem möchten wir Ihnen Peter Gundel, unseren Metallurgen, vorstellen. Mit über 35 Jahren Berufserfahrung in der Oberflächenhärtung trägt er maßgeblich zur Reduzierung der Umweltbelastung bei.
Des Weiteren freuen wir uns, Ihnen Brandon Zembrodt als neues Mitglied unseres US-Teams vorzustellen. Sie haben die Gelegenheit, ihn persönlich auf den kommenden Messen wie der PackExpo in Chicago und der Elmia in Schweden kennenzulernen!
Viel Spaß beim Durchlesen des aktuellen Newsletters. Seien Sie gespannt auf weitere Neuigkeiten von Expanite!
Ausgezeichnete Ergebnisse beim Galling-Test mit SuperExpanite-Härtung bei martensitischem Edelstahl
Hochwertige Materialien brauchen erstklassige Lösungen.
Basierend auf den Ergebnissen des standardisierten ASTM 98-Verschleißfestigkeitstests, zeigt der SuperExpanite Oberflächenhärtungsprozess bei dem martensitischen Edelstahl 1.4021 herausragende Ergebnisse! Diese beweist, dass Expanite überlegene Lösungen zur Verbesserung der Verschleißfestigkeit von Edelstahl bietet.
Sprechen wir gerne über unsere Innovativen Verfahren!
Konformitätserklärung für metallische Material mit Lebensmittelkontakt
Wir freuen uns, Ihnen mitteilen zu können, dass die Expanite-Oberflächenhärtung einen anspruchsvollen Test in Kontakt mit Lebensmitteln bestanden hat. Ihre herausragende Verschleißfestigkeit bietet rostfreien Edelstählen sichere Lösungen für den Einsatz im Lebensmittelbereich.
Haben giftige Chemikalien einen Platz in der Lebensmittel- und Getränkeindustrie?
Die Hartverchromung existiert seit über 100 Jahren. Leider erfordert diese altbewährte Technologie eine Reihe hochgiftiger Chemikalien, darunter hexavalentes Chrom, eine Substanz von sehr hoher Besorgnis gemäß der europäischen REACH-Verordnung.
Immer mehr Hersteller in der Lebensmittel- und Getränkeindustrie setzen auf Expanite, da sie auf die Einhaltung von Vorschriften, Umweltverantwortung und Sicherheit großen Wert legen. Schließen Sie sich dieser Entwicklung an
Geschrieben von Mia am . Veröffentlicht in Presse.
(Artikel auf Englisch)
Corrosion-resistant stainless steel is widely used in industry and trade due to its outstanding properties. Despite its numerous advantages, particularly its resistance to corrosion in numerous media, stainless steel also has considerable weaknesses that sometimes severely limit its application. One of these weaknesses is its susceptibility to cold welding or galling, which can occur particularly with screw connections. Surface hardening offers a solution to this problem.
Galling on stainless steel
Galling can be favored by various aspects, such as insufficient surface hardness, excessive roughness, or lack of lubricants. Nevertheless, fasteners are essential in many applications to allow for particularly frequent assembly and disassembly, or high tightening torques. It is therefore important to carefully tailor the properties of such elements.
When fasteners are jammed due to galling, their removal can turn out to be an enormous challenge, especially if it needs to be done without damaging the affected bolt or destroying the associated nut.
Surface hardening: the key to the solution
Fig.1: Generic image of a cold-welded screw connection
Surface hardening, a process in which only the surface layer (few to tens of microns) of a workpiece is hardened, has been proven to significantly improve the seizure behavior of stainless steel screws (Figure 1). The diffusion-based process increases the hardness of the surface through solid solution hardening and subsequently reduces its susceptibility to plastic deformation. Depending on the material, the corrosion resistance is maintained or even improved, and the stiffness of the base material is not impaired.
The Process
Surface hardening is not an applied coating, but a diffusion-based thermo-chemical surface hardening process. Although classic processes for the surface hardening of corrosion-resistant stainless steels have been available to the industry for some time, their application has two main disadvantages: firstly, all classic processes such as salt bath processes are known to reduce corrosion resistance. On the other hand, the hardness values of stainless steels usually hardened with nitrogen or carbon drop very quickly, i.e. the hardening depth is only a few micrometers and the underlying base material is very soft, which can potentially lead to the egg-shell effect.
In contrast, Expanite has developed its proprietary technology (SuperExpanite®) having solved those shortcomings as a priority. With our technological process not only the outermost layer but also the underlying material is hardened to a greater depth which also contributes to an improvement in corrosion resistance in many cases.
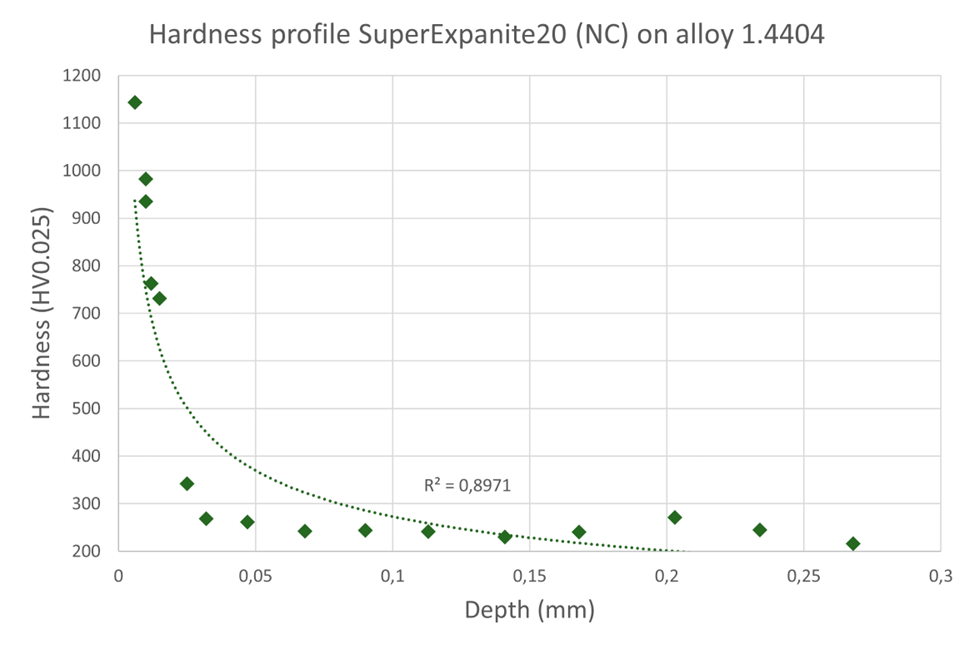
In many cases, a two-stage process is used in the Expanite’s treatment for stainless steels, in which nitrogen is introduced deep into the surface area in the first step called ExpaniteHigh-T (high-temperature process), whereby the material is hardened to approximately 300 HV for austenitic materials and 850 HV for alloys with martensitic structure to a depth of up to 1 mm. In the second process step, ExpaniteLow-T (low-temperature process, see micrograph in Figure 2), the workpiece is heated to temperatures below 500°C and the surface layer is hardened to 1100-1300HV at a hardening depth of 5-30µm (depending on the solution). The hardening is achieved by incorporating large amounts of interstitial carbon and nitrogen.
By combining the two process steps, the so-called eggshell effect, which occurs in most surface hardening processes, is avoided. This offers a decisive advantage for numerous applications that require improved load bearing capacity. The hardness profile can be seen in Figure 3.
Fig. 2: Micrograph of expanded austenite layer created with ExpaniteLow-T process (as a part of SuperExpanite product) on AISI 316L alloy.
Fig. 3: Hardness profile of AISI 316L. Below the extremely wear-resistant surface layer (produced in the ExpaniteLow-T process, approx. 1.200 HV) lies a medium-hard transition layer (250-300 HV), which is created in the ExpaniteHigh-T process. Power curve fitted for visual aid.
Wear resistance
To test wear resistance, Expanite tested some 316L samples hardened using its SuperExpanite® process to ASTM standard G 133. In this procedure (see Fig. 4), the SuperExpanite® treated test specimen is subjected to the reciprocating motion of 100Cr6 counterpart, under a contact pressure of 25N. The wear volume is determined after a sliding distance of 100 meters. The results are shown in Fig.: 2. The 316L sample with SuperExpanite® is 125 times more abrasion-resistant than the untreated sample.
Fig. 4: Wear measurement according to ASTM G133
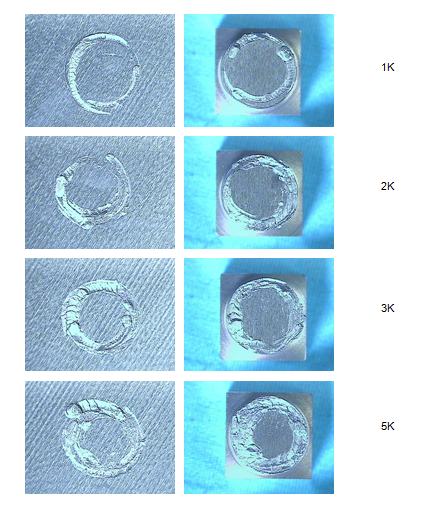
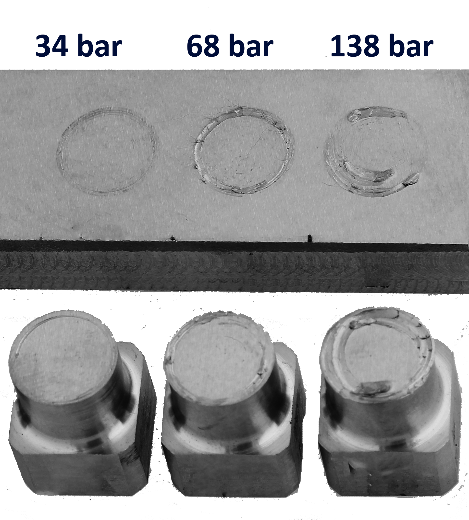
Following the ASTM G133, an ASTM G98 galling test (cold wear) was carried out with test specimens made of AISI 316L, the results of which are shown in Figures 5 and 6. In comparison to the unhardened test specimens, which already exhibit galling at a contact pressure of 35 bar, the test specimens hardened with SuperExpanite® do not show any galling even at a contact pressure of 2758 bar. Even though the first plastic deformations occur at this pressure due to the yield strength being exceeded. The risk of galling is therefore eliminated in the case of both friction partners being hardened.
Fig. 5: Untreated AISI 316L test specimens after ASTM G98
Fig. 6: SuperExpanite treated AISI 316L test specimens after ASTM G98
Corrosion resistance
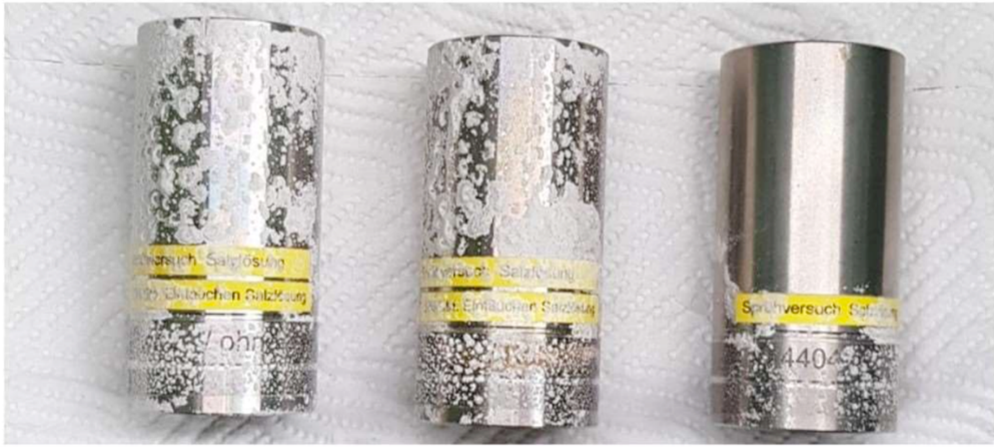
Although the basic intention of conventional surface hardening processes is to produce harder surfaces, this is usually at the expense of corrosion resistance. This is where the Expanite process comes in. Tests have shown that 316L samples hardened with SuperExpanite® can spend up to 1,000 hours in a salt spray chamber without showing signs of corrosion (see figure 7).
Fig. 7.: Results of the salt spray test on SuperExpanite hardened 316L alloy part (far right) as compared to competitors’ solutions
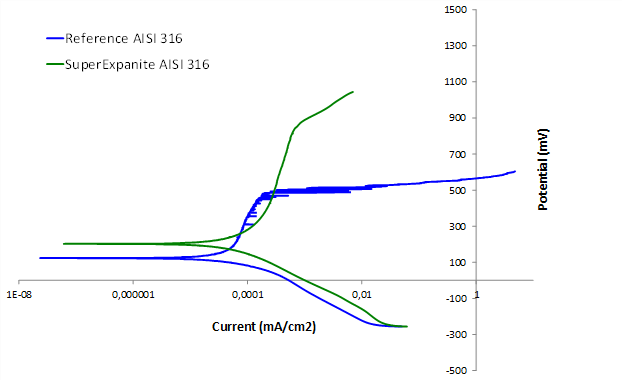
In some cases, the pitting corrosion resistance can even be significantly increased by the Expanite surface hardening process, even beyond the level of the unhardened base material. (Fig. 8). This effect is caused mainly by the large amount of nitrogen dissolved in the surface layer. A common formula for calculating the pitting resistance equivalent number (PREN) for alloys not containing tungsten, is given below (Eq. 1). It is easy to notice a relatively large 16x modifier in front of the nitrogen content expressed in weight percent (wt. %). This means that even small amounts of nitrogen have a significant positive influence on pitting resistance.
Eq. 1: PREN = %Cr + (3.3 x %Mo) + (16 x %N)
With the assumption of applicability of eq. 1 for large amounts of dissolved nitrogen [1], usually between 5 and 13 wt% [2], the PREN number can be calculated. For the AISI 316L alloy the calculated PREN numbers then range from around 100 even up to 230. A minimum of 4-fold increase over untreated material which has a PREN number of around 24. The underlying ExpaniteHigh-T zone can be characterized with PREN number of around 30, providing additional improvement even if the case hardening have been damaged or worn down.
A potentiodynamic polarization curve for SuperExpanite treated and reference AISI 316 material is shown in Figure 8. This test is a common tool used to evaluate the pitting corrosion potential and characteristics of a metal. There are several highlights that can be derived from the graph, showing the undeniable positive influence of SuperExpanite treatment on the pitting corrosion resistance of austenitic alloys.
Firstly, the open circuit potential of SuperExpanite treated sample is around 100mV higher than for the reference, suggesting better corrosion resistance in the absence of galvanic coupling. The polarization curve of the reference material also shows a much narrower passive region, that is characterized with many intermittent peaks (rugged line). Those lines indicate a sudden increase in current density (increased corrosion rate) and subsequent repassivation – initial pit formation. The plot obtained for SuperExpanite sample is free of those irregularities, and the material stays in the passive zone for potentials almost twice as large, with much more gradual decline towards the breakdown potential.
Fig. 8: Pitting resistance of AISI 1.4401 in seawater
Environmentally friendly
Despite their widespread use, conventional surface layer hardening processes have various disadvantages. Harmful chemicals such as fluorides, chlorides, molten salts etc. are used. SuperExpanite®, on the other hand, which is produced using the two-stage process described above, is characterized by an environmentally conscious approach. Without the use of harmful chemicals, and no polluted wastewater Expanite represents an environmentally friendly and sustainable alternative.
Summary
To summarize, the nitrocarburizing process specially developed by Expanite delivers excellent results in terms of both hardness and corrosion resistance for all stainless steel materials, not just limited to individual alloys. The process is therefore recommended for all types of stainless steel screws and fittings to extend the service life of the corresponding components and thus ensure increased product safety and interchangeability.
About Expanite
Expanite is a Danish company specializing in heat treatment and surface hardening of stainless steel and titanium. Expanite has established itself as a pioneer and trusted partner in the industry. The sustainable and patented surface hardening processes improves galling, wear and corrosion resistance on stainless steel and titanium parts in a wide range of applications and industries
The company has its head office in Hillerød near Copenhagen and service centers and licensees in the USA, Germany, Korea, and China. Expanite’s DNA is based on sustainable solutions to extend the life of components made of stainless steel, titanium, and other high-value alloys – and the business model allows for license agreements whereby customers may implement the technology in their production lines. www.expanite.com.
We do not have any open positions right now, you are always welcome to send us an unsolicited application. Please send your application directly clicking below.