Diamond-like carbon or DLC coatings are today used in many areas where excellent friction properties and good wear resistance are required on component surfaces. The DLC layers applied by complex, time-consuming and costly PVD or PACVD processes are usually only a few micrometres thick. If the part also is required to be corrosion-resistant, making the use of stainless steels mandatory, the DLC system has some weak points. The soft stainless steel as the carrier medium and the correspondingly high hardness gradient to the thin DLC layer promote the eggshell effect this might lead to a defect in the coating, and it will easily start peeling off.
Expanite (Copenhagen, Denmark) offers state-of-the-art solutions for surface hardening treatment of stainless steels and titanium. With Expanite’s processes, it is possible to increase the material’s surface hardness tenfold while at the same time maintaining and even increasing its corrosion resistance.
The Expanite technology, specially developed for corrosion-resistant materials, offers a solution for austenitic, martensitic, ferritic and duplex stainless steels as well as for expensive nickel-based alloys such as Inconel and Hastelloy. The new special process ExpaniteHard-Ti, which the Expanite team of experts in Denmark has developed to market maturity in recent years, is used for titanium materials.
Diffusion hardness layer
Surface hardening of Expanite brings the solution using a gas-based diffusion process to store carbon and nitrogen deep in the component surface. This guarantees a better load-bearing capacity and efficiently counteracts the eggshell effect. If defects occur in the hardness layer while the part is in use, this does not lead to further flaking because, in contrast to the applied DLC layer, the Expanite technology is a diffusion hardness layer that is coherent with the base material.
Environmentally friendly
In addition to technical and commercial advantages, the sustainability of the Expanite process is playing an increasing role for customers. The gas-based diffusion process is significantly more energy-efficient and environmentally friendly than comparable wear protection processes and, thanks to the treatment in vacuum, no time-consuming cleaning of the parts, e.g., with aggressive chemicals, is necessary after hardening with the Expanite process.
“We have already replaced the classic DLC coating in various applications, from the typical running and sealing surfaces in bearings, through pump components or knife edges to applications in medical technology,” explains Dr. Holger Selg, application expert and Expanite Sales Director DACH, and continues: “In some cases, the two technologies were also combined and a DLC layer was applied in addition to our Expanite hardness layer in order to obtain a very resilient system.”
With more than 20% of the turnover coming from hard chrome replacement projects, Expanite, the Danish pioneer within surface hardening of stainless steel, is on its way to position itself as one of the most used alternatives for hard chrome plating.
Finding a replacement for hard chrome plating can be challenging, and with EU regulations lowering the limit value for hexavalent chromium, the industrial markets need to find alternatives. Hard chrome plating, in various forms, has been one of “the standards” to improve resistance towards wear and corrosion for stainless steel components. And as new solutions are required, Expanite’s hardening technologies have documented their effectiveness within the automotive, pumps, valves and food processing equipment markets.
Sustainable Solutions, Diffusion vs. Coatings
Unlike a hard chrome coating, where the electrolyte used during processing may contain hexavalent chromium ions (Cr6+), which are hazardous to human health and environmentally harmful, the Expanite treatments involves only nitrogen and carbon atoms. This makes Expanite an environmentally friendly and sustainable process.
Expanite effectively removes the native oxide film covering stainless steels during the first steps of the gas process without adding any aggressive chemicals, and this allows controlled diffusion of carbon and nitrogen atoms in the underlying stee, thereafter.
Nitrogen/Carbon Diffusion Replacing Hard Chrome Plating
“More than 20% of the parts we are processing today with the Expanite process are replacements for hard chrome plating,” says Thomas Abel Sandholdt, CEO at Expanite. Whether it’s the valve parts of a fuel injector within automotive, a bushing for marine engines or the rotor for a large pump, they have all experienced the benefits of choosing a diffusion process with no risk of coatings cracking or inhomogeneous hardening zones. And along with that comes the compliance with the EU Reach program on reduction of Cr6+ as well as the fundamental decision to move towards more sustainable solutions.
Commenting about replacing hard chrome with Expanite, Sandholdt highlights opportunities in the automotive industry with valve components. “Independently of each other, three major suppliers to the automotive industry approached Expanite,” says Sandholdt. “They all produce fuel injectors with valve components in ferritic stainless steel, which traditionally were hard chromed plated. All three were facing issues such as wear, general quality problems and high cost.
And they all found various solutions within the Expanite toolbox. The first of the three projects went into serial production in January 2020, while the two other projects are scheduled to begin serial production in 2021 and 2022. “As we are often our customers´ biggest secret, many will not allow us to reveal that we actually have helped them change from hard chrome plating.”
Competitive Cost
From the first look, Expanite hardening technology might seem costly compared to hard chromium plating. However, Sandholdt says that he is convinced the price difference will equalize, once total life cycle cost and performance are taken into account. According to Sandholdt, “The proof lies in the decisions made by so many of Expanite’s customers.”
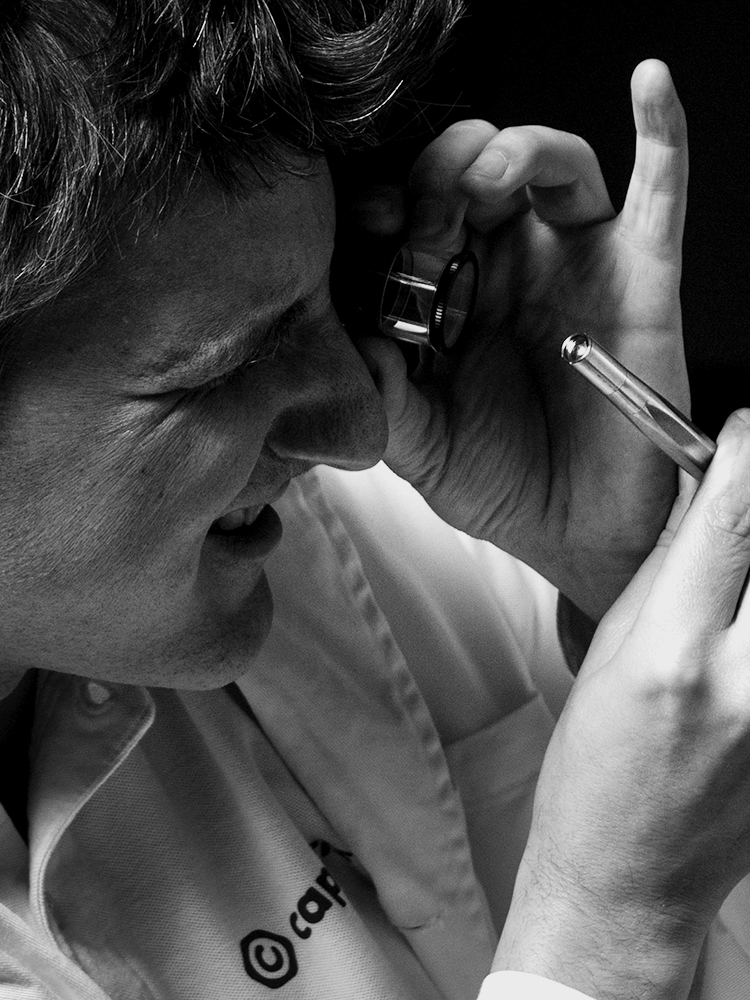
With the ambition of creating the ultimate fountain pen, combining innovative production methods with advanced materials, Capillaris reached even further by seeking Expanite’s help with hardening the surfaces of the unique writing tool. The result is a fountain pen designed by aerospace engineer Zsolt Pataki, made from a solid titanium bar for the ultimate weight, look and feel, hardened by ExpaniteHard-Ti making it long-lasting and virtually unscratchable.
Hunting for the superior scratch resistance.
Aerospace engineer Zsolt Pataki got a crazy idea; he wanted to create a unique fountain pen using his experience from aerospace in design, materials, and manufacturing. He chooses titanium grade 23 from the very beginning of the development process, but also knew that he wanted to go further. Mr. Pataki states: “In my search for increased wear resistance of the titanium, I was eager to avoid the hurdles of a coating; adding layers affecting the dimensions combined with the risk of layers chipping off – as I preferred a monolithic design with the original titanium surface instead of a coating”.
In the search for alternatives to coating, Mr. Pataki attended a webinar with Expanite presenting their unique hardening solution for titanium. “I soon realized that the ExpaniteHard-Ti process was the only matured and commercially available interstitial hardening technology for titanium. The webinar combined with the details of the technology on their web site helped me to develop realistic expectations and I reached out to them”, Mr. Pataki continues
The solution
The ExpaniteHard-Ti process provides highly effective protection against wear and scratches. The method is not a coating process, hence all the drawbacks of coatings, including the risks of chipping/spalling off and inconsistencies in layers are completely avoided. In fact, it is the surface of the material itself, which is hardened. The ExpaniteHard-Ti process has a significantly greater level of protection against scratches than that afforded by the hardness of the base material and the hardened parts retains the design colour or as Mr. Pataki describe it: “I tried hard to scratch the pen after the process, but it is practically impossible – I made before and after comparison and the results are spectacular; the pen is now virtually unscratchable”!
Professional knowledge sharing
Through the dialogue with the Expanite team, the optimal solution to increase scratch resistance of the fountain pen was found – Mr. Pataki states: “Throughout the whole process, the Expanite team has been very supportive and open to discuss questions and possible issues ensuring that I got exactly the solution that suited my requirements for the pens and the fact that the results were much better than advertised in terms of case depth of the hardened zone!”
This article is a Q & A with Rune Strand regarding ExpaniteHard-Ti. Strand is project manager and material scientist at Expanite A/S, and he holds an MSc in material science and manufacturing. He has spent most of his career in the field of surface hardening and heat treatment of stainless steel.
Why is surface hardening of titanium relevant?
Surface hardening of titanium is relevant simply because titanium and titanium alloys by nature are soft and will exhibit poor wear resistance. This contradicts something we often hear: “Why would you need to harden titanium? Isn’t that really tough?” The truth is that titanium and titanium alloys are actually very tough, but toughness, hardness and strength are often confused with each other. In general terms, hardness is the feature that will give a material wear resistance, and titanium by itself is not very hard.
Where do you see a hard titanium surface being beneficial?
Basically, the sky is the limit, both figuratively and literally. The aerospace industry uses an abundance of titanium, and any part that exhibits wear will benefit from our surface-hardening technique. Currently, we have seen the highest demand from the Swiss watch industry, where the goal is to make titanium watch parts more scratch-resistant. We also see the applicability in the emerging 3D/additive manufacturing (AM) market as well as medical devices.
What methods exist today to increase surface hardness and improve wear resistance?
The most typical methods are anodizing and TiN coatings. Both of these are coating-type methods where the hardening effect is achieved by forming “something else” on the surface. This “something else” will have a good hardness and probably also decent wear properties. The drawback of these types of treatments is that there is a great risk of delamination of the coating, simply because it is “something else” than the underlying structure. Delamination can be initiated by temperature fluctuations, hard impacts, etc. and is often referred to as “the egg-shell effect.”
Is ExpaniteHard-Ti a coating?
ExpaniteHard-Ti is far from a coating. The process relies on diffusion of interstitial atoms into the original microstructure of titanium/titanium alloys.
What are the typical achieved specifications for hardness and depth?
Typically, we achieve 30 μm and 1000 HV hardness. The graph shows the total elimination of wear in a standard ASTM G133 pin on a disk wear test.
What are the benefits of an interstitial diffusion hardening process such as ExpaniteHard-Ti?
The most pronounced benefit from a process like ExpaniteHard-Ti lies within the nature of the process – diffusion. Diffusion of interstitial atoms into an existing structure creates compressive stresses that result in a hardness increase. This completely eliminates any discussion about adhesion to substrate and delamination of the hardened zone because it is a part of the original structure and not “something else” on top.
Contrary to austenitic stainless steel, heat treatment of titanium is an important parameter to obtain certain mechanical properties. How do you accommodate this?
We can achieve basically all heat-treatment conditions simultaneously with the hardening process itself. If it is not possible to have the specific heat-treatment condition that is required within the parameters of our hardening process, then we do the specific heat treatment either before or after diffusion-hardening a part.
Are there any drawbacks of your process?
There are a couple, namely a slight discoloration and a little distortion. The discoloration can be omitted, and we are currently working on a modified version to commercialize the change in process details that is necessary. Concerning the distortion that can happen to parts when surface hardened, it is actually mostly due to a temperature in the treatment exceeding the alpha/beta transus temperature. This issue is also addressed in the new developments, however, where a temperature well below the alpha/beta transus temperature is used.
In what segments or fields are you seeing requests for such a process?
Mostly jewelry, but both the aerospace and medical industries are starting to show some real interest.
What is the matureness of said process?
We are ready to mass produce.
How do you provide the technology (on-site/service provider)?
Expanite offers two solutions: as with a normal service provider, where the customer sends us the goods, we harden and ship back; or as an onsite solution, where a customer can buy a furnace (preferably through a specific furnace manufacturer) and run the ExpaniteHard-Ti process on a license agreement.
What are typical lead times/cycle times?
Typically, it will not take more than 24 hours to do the actual hardening process. Expanite has a standard lead time of nine working days.
Do you see any upcoming applications for your technology?
Basically, any 3D-printed parts seem to be next big jump in the application of our ExpaniteHard-Ti process, where the benefits of the hardened zone can reach far beyond just the surface.
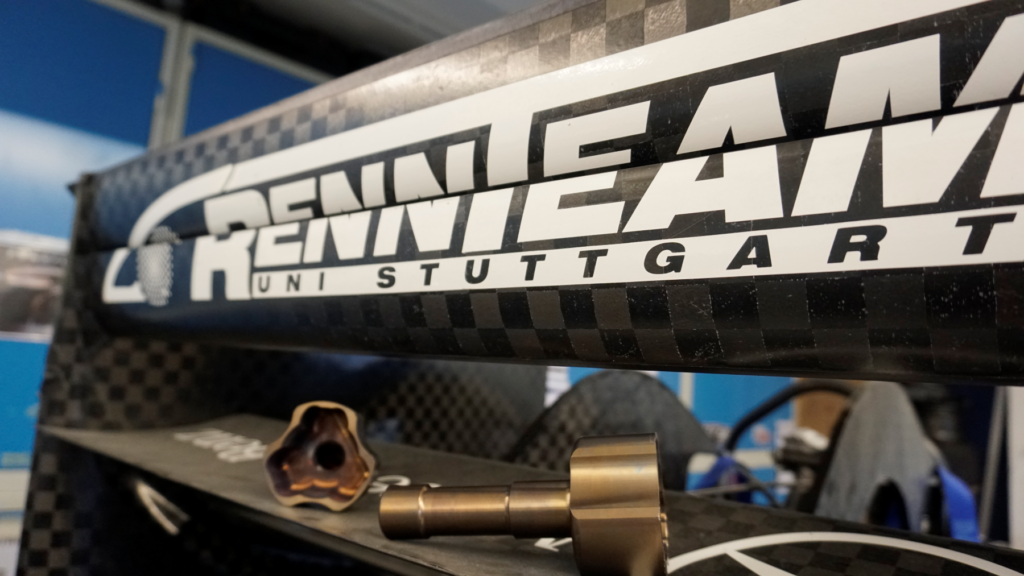
Expanite, the surface hardening specialist, has consulted and advised the students at the RennTeam Uni Stuttgart in identifying and solving some of their challenges with wear on the titanium parts in their racing car. The Rennteam Uni Stuttgart takes part in the Formula Student racing series, a competition for young engineers across Europe, as well as being involved in other international competitions.
The young constructors of the Rennteam Uni Stuttgart are constantly striving to optimize the construction process including the use of materials and spend almost all their time in constructing and testing the cars to prepare for competitions.
To increase the performance including lowering the weight of the race car, the students changed some of the parts to titanium but were faced with problems related to wear parts due to low surface hardness and they decided to contact Expanite for possible solutions.
The Expanite material experts proposed to surface harden the critical titanium parts including parts of the power train, sitting between the differential and the drive shaft with the ExpaniteHard-Ti process. The Expanite hardening makes the use of light-weight titanium parts possible therefore resulting in increased efficiency and significant weight reduction.
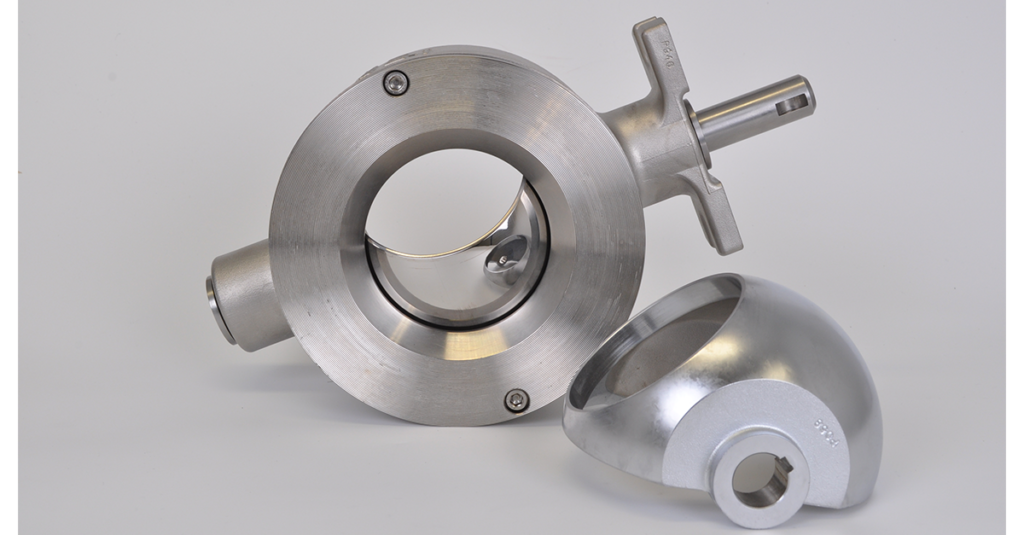
LIAG LÄUFER is a specialist in hygienic shutter valves and pigging systems. The products are designed to meet the highest safety demands in the food industry and must withstand signicant abrasive wear and corrosion aggressive environment.
Their stainless steel cones were originally specied with hard chrome plating. Due to the potential health risks however, hard chrome plating is increasingly prohibited in the food industry. LIAG LÄUFER needed to find an alternative. In their attempt to solve these challenges LIAG LÄUFER tried different surface hardening solutions, which all failed, including a commonly used carburizing process, which caused corrosion after short time in use
Their stainless steel cones were originally specied with hard chrome plating. Due to the potential health risks however, hard chrome plating is increasingly prohibited in the food industry. LIAG LÄUFER needed to find an alternative. In their attempt to solve these challenges LIAG LÄUFER tried different surface hardening solutions, which all failed, including a commonly used carburizing process, which caused corrosion after short time in use
LIAG LÄUFER finally tested Expanite and found a hardening solution that effectively reduces wear and galling, and at the same time improves the corrosion resistance of the parts.
LIAG LÄUFER is determined to offer environmentally sustainable solutions to comply with the industry demand to exclude chrome in the food industry. Expanite hardening solution is a diffusion-based process and therefore significantly more environmentally friendly and sustainable compared to other hardening methods.
The patented Expanite process doesn’t add anything to the material (besides nitrogen and carbon), it just makes the surface harder as much as 10 times harder.
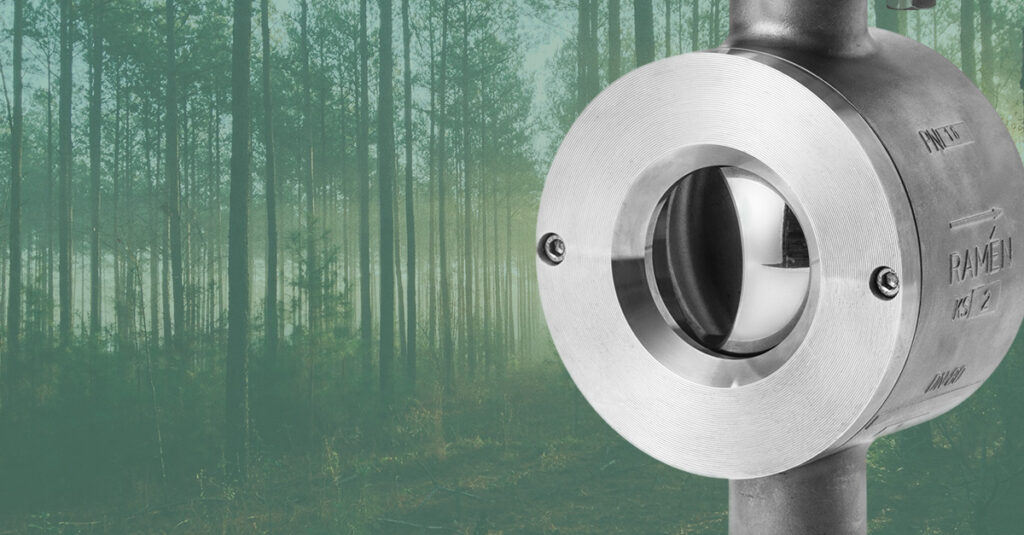
Sweden’s Ramén Valves is a highly respected supplier to equipment manufacturers in industries as varied as food & beverage and mining & minerals. As a successful business of almost 80 years, it is adept at planning ahead to navigate a changing landscape. Part of this is an active sustainability programme to improve environmental performance, keep clear of regulatory risk and remain relevant among customers.
With heightened awareness of the health and environmental dangers of hexavalent chromium and tightening REACH regulations, Ramén Valves knew it would need an alternative to hard chrome plating. But which alternative was best, not only in terms of hardening but also sustainability?
Magnus Alfredsson, strategic purchasing manager at Ramén Valves, led the investigation. He lays out the company’s requirements. “Whatever process we selected it would have to harden at least as well as hard chrome plating, protect people and planet from toxic chemicals, and reduce our use of resources.”
“On wear performance, they showed us a decisive test that demonstrated they could deliver around 300 times less wear than standard vacuum hardening, Magnus Alfredsson – Strategic Purchase Manager, Ramen Valves.”
With these clear objectives, Magnus started to speak with suppliers. “We looked at all the various technologies,” he says. “It wasn’t long before we found a strong candidate.”
Decisive wear performance
“Expanite was very good at answering our questions and providing information,” says Magnus. “On wear performance, they showed us a decisive test that demonstrated they could deliver around 300 times less wear than standard vacuum hardening.”
The Expanite process offered a further practical benefit that Ramén found valuable: its suitability in situations where hard chrome is unusable.
To illustrate the point, Magnus provides an example. “If we choose to make our valves in SST316L to ensure compatibility with the media, then the compatibility is preserved with Expanite. But with hard chrome plating the media interacts not with the base material but with the chrome layer. This can lead to corrosion, making chroming unsuitable.”
No harmful chemicals
Having confirmed the performance and suitability of Expanite’s process on paper, Magnus’ attention turned to sustainability.
“Expanite is one of the ways we can show we are reducing our footprint and differentiating ourselves from competitors. In other Nordic countries bigger companies are starting to ask about this too”, Stephane Blanchet – Sales Manager, Ramen Valves“Of course, reduced wear is a sustainability factor in itself because fewer parts need to be replaced, but we also wanted a safe, low resource process. Hard chrome plating uses harmful chemicals like chromic acid, sulfuric acid, lead, lead chromate and lead oxide. It causes toxic waste. We were happy to discover that Expanite uses no harmful chemicals, only small amounts of nitrogen, ammonia and propene, and produces no toxic waste. It fitted our requirements perfectly.”
Making the switch
With Expanite identified as the best potential replacement for hard chrome, it was time to put it to the test.
“We started out with smaller internal parts, then larger components and applications in really aggressive environments,” says Magnus. “Everything went smoothly, which gave us the confidence to begin the switch out of hard chrome plating. The whole process took almost a year.”
Attracting new customers
The Expanite process is part of Ramén’s strategy for attracting new customers. “In Sweden customers are asking about our environmental impact,” says Ramén’s sales manager Stephane Blanchet. “Expanite is one of the ways we can show we are reducing our footprint and differentiating ourselves from competitors. In other Nordic countries bigger companies are starting to ask about this too.”“Looking at the future with all the regulations coming we are ahead of our competitors, and it will be expensive for them to catch up. We are already four years into our partnership with Expanite and expanding our cooperation”.
A safer, healthier future
Ramén’s CEO Per Wennesten has the final word. Although the switch from hard chrome plating to Expanite has strengthened his company, for him it’s more than business, it’s personal.
“Who do you want to be at work?” he asks. “The choices you make at work may have an even bigger impact on the world than the choices you make at home. Both choices are important so be sure to make a choice. We’re proud of our choice and that we’re contributing to a safer, healthier future for everyone.”
About Expanite
Expanite offers state-of-the-art solutions for surface hardening treatment of stainless steels and titanium.
With Expanite’s processes, it is possible to increase the material’s surface hardness tenfold while at the same time maintaining and even increasing its corrosion resistance. Expanite is a global organization with a combined development and production facility near Copenhagen, Denmark, and hardening capacity in both US, Germany, Korea and China. Expanite’s solutions are flexible and can be introduced directly into a customer’s own production line as part of a licensing arrangement. Learn more on www.expanite.com.
The REACH regulation was established by the European Union to better protect health and the environment from the dangers of chemicals. REACH, an acronym for Registration, Evaluation, and Authorization of Chemicals, defines how and under which conditions specific chemicals can be used within the EU.
REACH regulation
Although this regulation came into effect in 2007, it gained more attention in 2013 when Chromium Trioxide (Chromium(VI) oxide) was added to the list of substances requiring authorization because of its carcinogenic and mutagenic properties.
Chromium(VI) oxide stands out from other substances on this list because of its wide range of applications. It is primarily used for surface treatments, whether for enhanced corrosion protection or the production of visually attractive surfaces. As a result, many industries, such as the electroplating industry and mechanical engineering, are feeling the impact of this regulation.
Coating
In general, coating methods that can prevent corrosion tend to add material and are often inconsistent in terms of the thickness of the applied layer. This can result in material accumulations on flat structures or material thinning at corners and edges where protection is reduced. Additionally, coatings may crack and peel off during significant expansion or contraction of the base material due to differences in the thermal expansion coefficient between the base and the coating. Complex contours with undercuts and small openings pose additional challenges, and certain coating methods are not compatible with these surfaces. Expanite takes a different approach to this process that avoids these issues.
The sustainable Expanite® processes:
A solution to the above-mentioned problems involving stainless steels is surface hardening. This is not a coating process but a diffusion-based surface hardening process. Traditional methods for surface hardening corrosion-resistant stainless steels have been available to the industry for some time. However, they mainly have two disadvantages: they reduce corrosion resistance, and the hardness value of steels hardened with nitrogen or carbon often decreases rapidly at the material core. This means that the hardening depth is only a few microns, and the underlying structure is very soft, which can potentially lead to an “eggshell effect.”
Expanite has developed a method that hardens not only the outermost layer, but also hardens the underlying material to a greater depth. In many cases, this also results in improved corrosion resistance.
The Expanite treatment for stainless steels involves a two-step process. In the first step (high-temperature process), nitrogen is introduced deep into the surface zone, allowing the material to achieve a hardening up to 1mm in depth ranging from approximately 300 HV (austenitic materials) to 850 HV (martensitic materials). In the second step, the so-called low-temperature process, the workpiece is heated to a maximum of 470°C, and the surface layer is hardened to a depth of 5-30μm, achieving 1100-1300HV (see photo 1), through the embedding of carbon and nitrogen. Combining these two processes prevents the aforementioned “eggshell effect” and offers significant advantages for different kinds of applications.
Photo 1: Expanded Austenite after the Process
Eco-Friendly
Despite its widespread use, hard chrome plating has several disadvantages. Harmful chemicals such as chromic acid, sulfuric acid, lead, lead chromate, and lead oxide are all used in the process. Additionally, it is largely inefficient with at least 70% of the electrical energy being wasted.
SuperExpanite®, the trade name for the layer produced in the Expanite’s two-stage process, stands out for its resource-saving approach. It neither consumes natural re-sources nor produces polluted wastewater. With a low energy consumption of only 1.9 kWh/kg of hardened stainless steel and without the use of harmful chemicals, it offers an environmentally friendly and sustainable alternative to hard chrome plating, which also extends the lifespan of fittings.
Photo 2: Furnaces for surface hardening stainless steel products
Ideal for Abrasive Media Due to Increased Hardness
Hard chrome coatings typically have a hardness of HV 300-1,400, whereas SuperExpanite achieves HV* 1,200±100. The increased hardness of materials treated with SuperExpanite therefore provides better wear resistance, making them perfect for applications involving abrasive materials.
Better Resistance to Galling
Both the SuperExpanite treatment and hard chrome plating produce a strong resistance to galling. However, the inherent cracks in hard chrome coatings can cause the tarnishing of the partner surface, which can lead to galling. By contrast, surfaces hardened with SuperExpanite are crack-free and resist galling.
A Broader Range of Applications Due to Improved Corrosion Resistance
The SuperExpanite treatment does not adversely affect the corrosion resistance of the base material; it can even enhance the corrosion resistance of certain materials, such as stainless steel 316L. Conversely, hard chrome plating produces a layer on the base material that may be incompatible with certain substances due to corrosion. For instance, sulfuric acid and phosphoric acid are not compatible with hard chrome coatings. However, stainless steel 316L or 254SMO, which many valve manufacturers supply as the standard, that is treated with SuperExpanite can be used with these substances depending on the concentration and temperature. This means that the SuperExpanite treatment can be utilized in situations where the use of hard chrome is prohibited or technically impracticable.
Extended Lifespan in Abrasive Applications
The SuperExpanite treatment can be used on components that are not traditionally hard-chromed, such as valve housings. The increased hardness of the SuperExpanite process results in a longer lifespan when valves are used in highly abrasive applications.
Summary
With its technology hardened surface layers, Expanite offers a more environmentally friendly alternative to hard chrome that boasts a lower energy consumption, higher hardness, and better resistance. Expanite also provides a longer lifespan in abrasive applications and a more robust surface treatment without the typical risks of hard chrome plating.
About Expanite
Expanite offers state-of-the-art solutions for surface hardening treatment of stainless steels and titanium.
With Expanite’s processes, it is possible to increase the material’s surface hardness tenfold while at the same time maintaining and even increasing its corrosion resistance. Expanite is a global organization with a combined development and production facility near Copenhagen, Denmark, and hardening capacity in both US, Germany, Korea and China. Expanite’s solutions are flexible and can be introduced directly into a customer’s own production line as part of a licensing arrangement. Learn more on www.expanite.com.
(Article en anglais)
Material optimization – The nitrocarburizing process developed by Expanite enhances both the hardness and corrosion resistance of stainless steel materials – and not just for individual alloys. Therefore, the process is also recommended for medical device applications. It extends the lifespan of the respective application, thereby increasing patient safety and reduces cost.
Because of its unique properties and versatility, Stainless steel is an essential material for medical devices and implants that frequently encounter liquids and tissue. The corrosion resistance of stainless steel guarantees an extended lifespan and prevents the development of rust or other forms of damage that could compromise the functionality and safety of the medical products.
For decades, corrosion-resistant stainless steel has been extensively used in the field of medical technology and is offered in a diverse array of alloy variations in the market. Numerous companies opt for these materials due to their corrosion resistance, with particular emphasis on the austenitic and duplex variants. Nevertheless, these options are challenged by their susceptibility to wear attributed to their relative low hardness, often resulting in issues such as galling.
Conventional techniques aimed to increase wear or galling resistance on stainless steel components come with a drawback – they often result in non-corroding steels becoming susceptible to corrosion post treatment. Coating methods designed to prevent this issue involve the application of material, but in numerous cases, they exhibit inconsistencies in terms of layer thickness. This inconsistency leads to the accumulation of material on flat surfaces, while corners and edges experience a reduction in the protective layer. Additionally, coatings can develop cracks during significant expansions or contractions of the underlying material due to the different thermal expansion coefficients of the base material and coating. Small openings present further challenges, as the coating process may not be effectively applied depending on the process used. Bypassing these hurdles has become the core objective of Expanite, the Danish provider of surface hardening technologies.
Enhancing Stainless Steel Performance
Addressing the aforementioned problems with stainless steels involves the application of surface layer hardening, a process distinct from coating that relies on diffusion-based surface hardening. While traditional methods of surface layer hardening for corrosion-resistant stainless steels have been available to the industry for some time, they inherently possess two primary drawbacks. Firstly, all conventional methods result I a reduction in corrosion resistance. Secondly, the hardness values of stainless steels typically treated with nitrogen or carbon experience rapid degradation, resulting in a shallow hardening depth in only a few micrometers. and the underlying structure is very soft, which could potentially lead to an eggshell effect. Consequently, the underlying structure remains quite soft, potentially leading to a fragile shell-like effect.
However, Expanite has pioneered its own FDA-compliant process that overcomes these limitations. In this process, not only the surface layer but also the underlying material is profoundly hardened. This specially developed nitrocarburizing method is a thermochemical process for steel, facilitating the diffusion of nitrogen and carbon into the workpiece’s surface. This achieves enhanced surface hardness, improved wear resistance, and heightened corrosion resistance Nitrocarburizing combines the benefits of both nitriding and carburizing with a single process.
Process Protects Workpiece from Wear and Corrosion
The Expanite treatment of stainless steels typically involves a two-step process. During the initial phase (high-temperature procedure), nitrogen is introduced deeply into the boundary zone. This results in the material being hardened up to around 1 mm, with hardness levels ranging from approximately 300 HV for austenitic materials to 850 HV for martensitic materials.
In the subsequent stage, referred to as the low-temperature procedure, the workpiece is gradually heated to a maximum of 470°C. This controlled heating enables the infusion of both carbon and nitrogen, effectively reinforcing the boundary layer to a depth ranging from 5 to 30 μ achieving hardness levels between 1100 and 1300 HV. Combining both process steps, the fragile eggshell effect is avoided.
To test wear resistance, Expanite conducted tests on several 316L samples that had undergone its proprietary hardening process, following the guidelines of ASTM standard G98. In this test, a ceramic test body is moved back and forth on a test specimen under a constant pressing force of 25 N. After a sliding distance of 100 m, the resulting wear volume is qualified. Remarkably, the sample treated with Super-Expanite exhibited wear resistance levels 125 times superior to those of the untreated sample.
While conventional surface hardening methods aim to enhance surfaces hardness, they frequently come at the cost of compromising corrosion resistance. This is precisely where our procedure steps in: Extensive testing has demonstrated that samples subjected to Expanite’s hardening process can endure up to 1000 hours in a salt spray fog chamber without exhibiting subsequent corrosion indications. In fact, surface hardening can occasionally elevate corrosion resistance to levels surpassing those of the untreated base material.
About Expanite
Expanite offers state-of-the-art solutions for surface hardening treatment of stainless steels and titanium.
With Expanite’s processes, it is possible to increase the material’s surface hardness tenfold while at the same time maintaining and even increasing its corrosion resistance. Expanite is a global organization with a combined development and production facility near Copenhagen, Denmark, and hardening capacity in both US, Germany, Korea and China. Expanite’s solutions are flexible and can be introduced directly into a customer’s own production line as part of a licensing arrangement. Learn more on www.expanite.com.
In recent weeks and months, Expanite has developed surface hardening solutions for the pump and valve market. The main problems in the past in these industries have always been wear and galling – all applications where either metal sealing is needed, or due to high operational temperatures (far above 300 °C) and/or corrosive environments, conventional coatings and most non-metallic bushings cannot be used.
Diffusion-based hardening technology
Even where special coatings may be applied in certain environments, heating and cooling cycles normally introduce a high risk of spallation due to different coefficients of thermal expansion. Customers seeking improved performance finally found a more advanced solution – the unique diffusion-based hardening technology of Expanite that is applicable to most commercially available corrosion-resistant alloys. Recently, the Expanite-technology has set a new standard for wear and galling on different materials such as conventional stainless steel (1.4404/AISI 316, Duplex 1.4462, Nitronic, 1.4980/Alloy A-286), Ni-based alloys (e.g. Monel® K500, Inconel® 718 and Hastelloy®) and Co-based alloys such as Stellite®. Stainless steel is, in many cases, used in valves for food and pharma applications, whereas Monel & Inconel are widely applied in chemically aggressive and harsh environments.
The new technology
Expanite’s hardening technology generates surface hardness values in the area of 900 to 1500 HV – on stainless steel, Co-based and many Ni-based alloys, thereby effectively preventing galling. Especially on relatively large valves used in the chemical industry and power plants, galling on shifting shafts (opening and closing the valve) made of Inconel and Monel has previously caused severe problems. Applying the Expanite-technology on these shafts prevents galling and thereby increasing the life-time of the valve components.
Unique test results
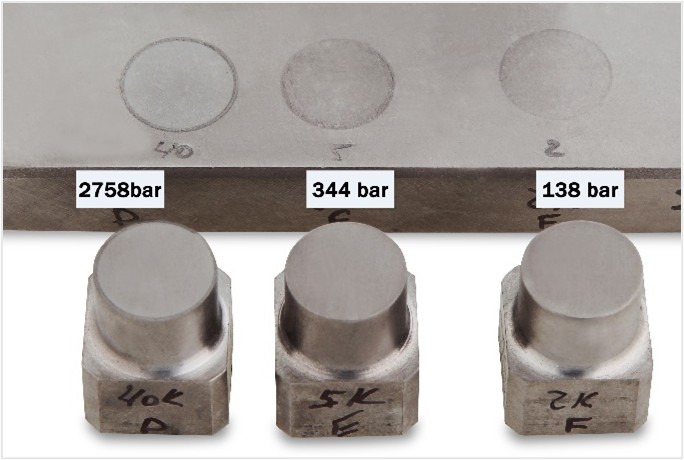
This has been impressively demonstrated by a test method for galling resistance (according to ASTM G98 test procedure) on an austenitic stainless steel (1.4404/AISI 316L), with and without Expanite surface treatment (cf. Fig. 1 &2).
Fig. 1: galling result on non-treated 316-material showing significant galling at relatively low contact-pressure
Fig. 2: galling result on Expanite-hardened 316-material showing absolutely no galling even at contact pressures well above yield strength
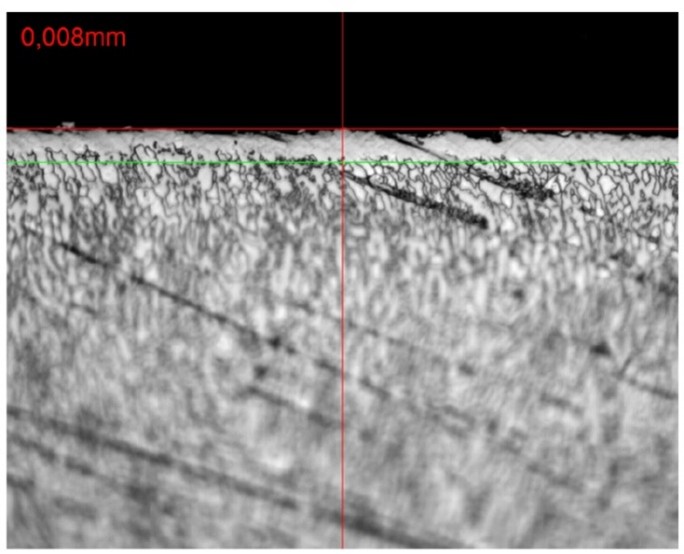
Fig. 3: light optical micrograph of an Expanite-hardened Inconel 718 evidencing a homogenous case-depth in the range of ca. 10µm. Surface hardness measurements reveal ca. 1,000 HV0.025
Fig. 4: light optical micrograph of an Expanite-hardened Stellite 1040 showing a hardened zone of ca. 8µm. Surface hardness measurements resulted in ca. 900HV0.025
Fig. 5: light optical micrograph of Expanite-hardened A 286 (1.4980) material. The case-depth can be tailored between 10 and 35µm, resulting in surface hardness of 1,200-1,500 HV0.05
About Expanite
Expanite offers state-of-the-art solutions for surface hardening treatment of stainless steels and titanium.
With Expanite’s processes, it is possible to increase the material’s surface hardness tenfold while at the same time maintaining and even increasing its corrosion resistance. Expanite is a global organization with a combined development and production facility near Copenhagen, Denmark, and hardening capacity in both US, Germany, Korea and China. Expanite’s solutions are flexible and can be introduced directly into a customer’s own production line as part of a licensing arrangement. Learn more on www.expanite.com.